
Do You Have Complete Visibility into Your Production Operations?
Without reliable machine data, production losses can remain hidden.
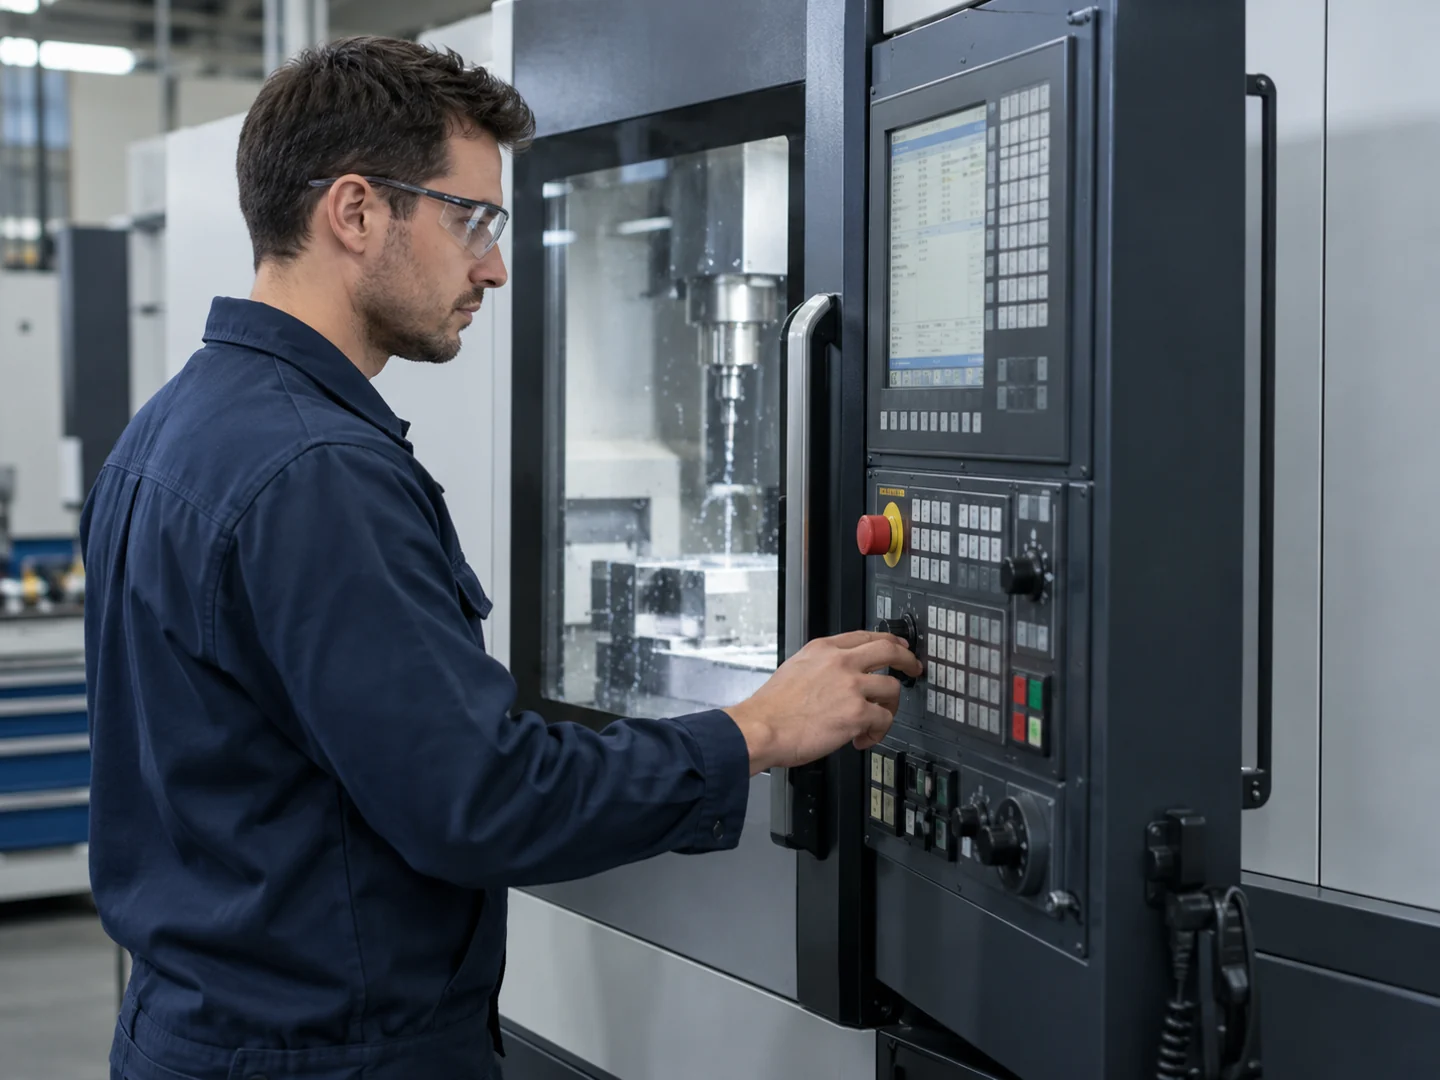
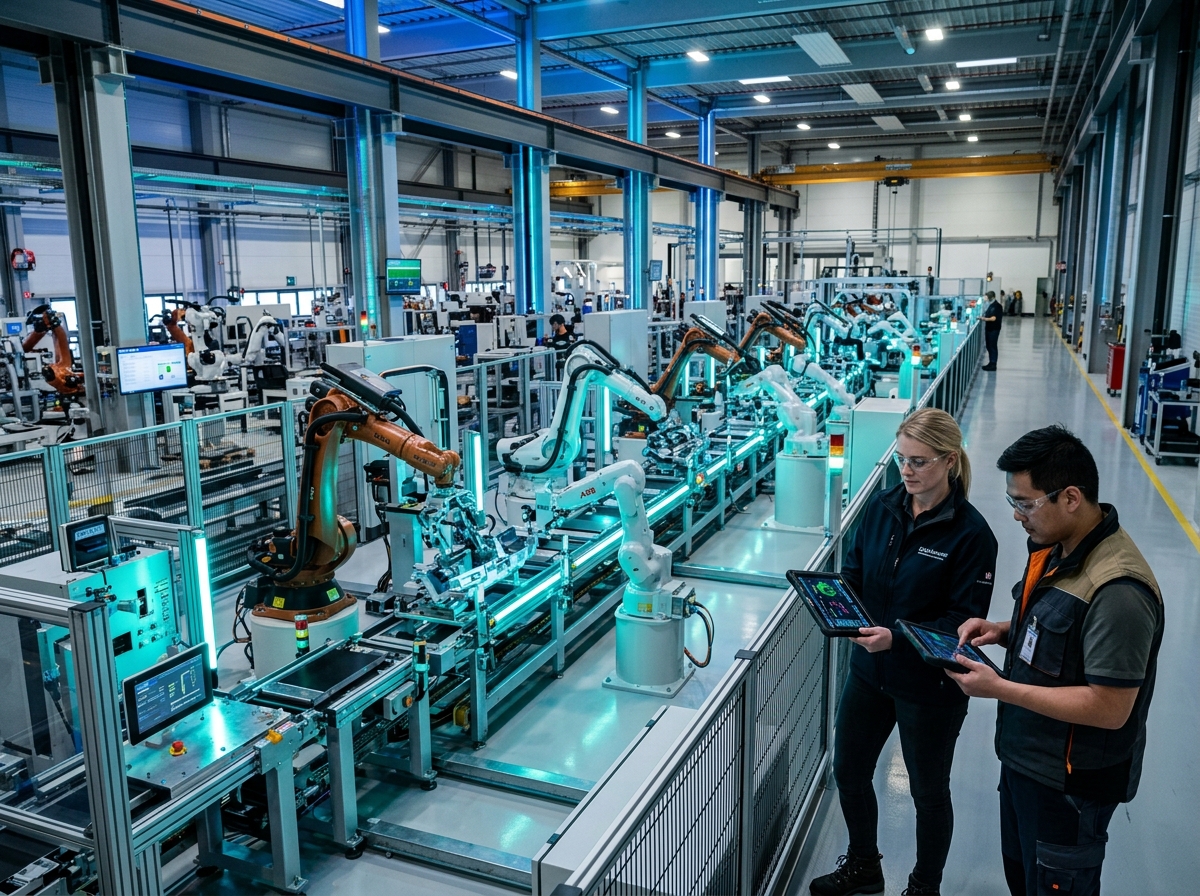
Machine & Production Monitoring System
MICROCIL's Industrial IoT monitoring approach connects machines, sensors and industrial data sources to a centralized monitoring platform. It transforms available equipment signals into useful information for production teams, maintenance engineers and factory management.
From individual machines to multiple production lines, the solution can be configured around your equipment, data availability and operational priorities.
From Connected Machines to Measurable Business Impact
Our solutions are designed for a wide range of industrial vehicles, machines and environments.
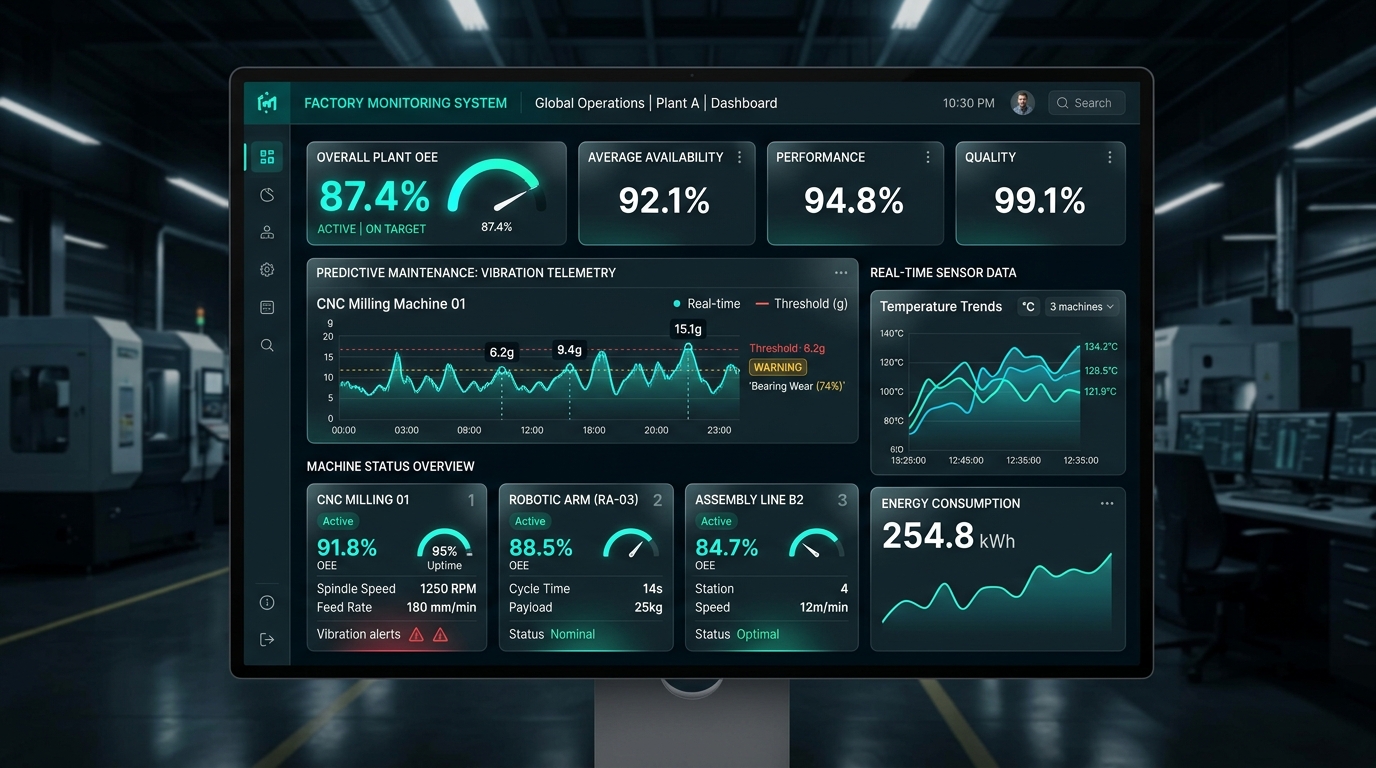
Real-Time Machine Monitoring
Live status, operating parameters and production counts.
Production Tracking
Track output, cycle time and shift-wise performance.
Downtime Analysis
Automatic stop detection with root cause insights.
OEE & Utilization
Understand machine availability, performance and quality.
Alerts & Diagnostics
Configurable alerts for abnormal conditions and failures.
Maintenance Insights
Support preventive and predictive maintenance.
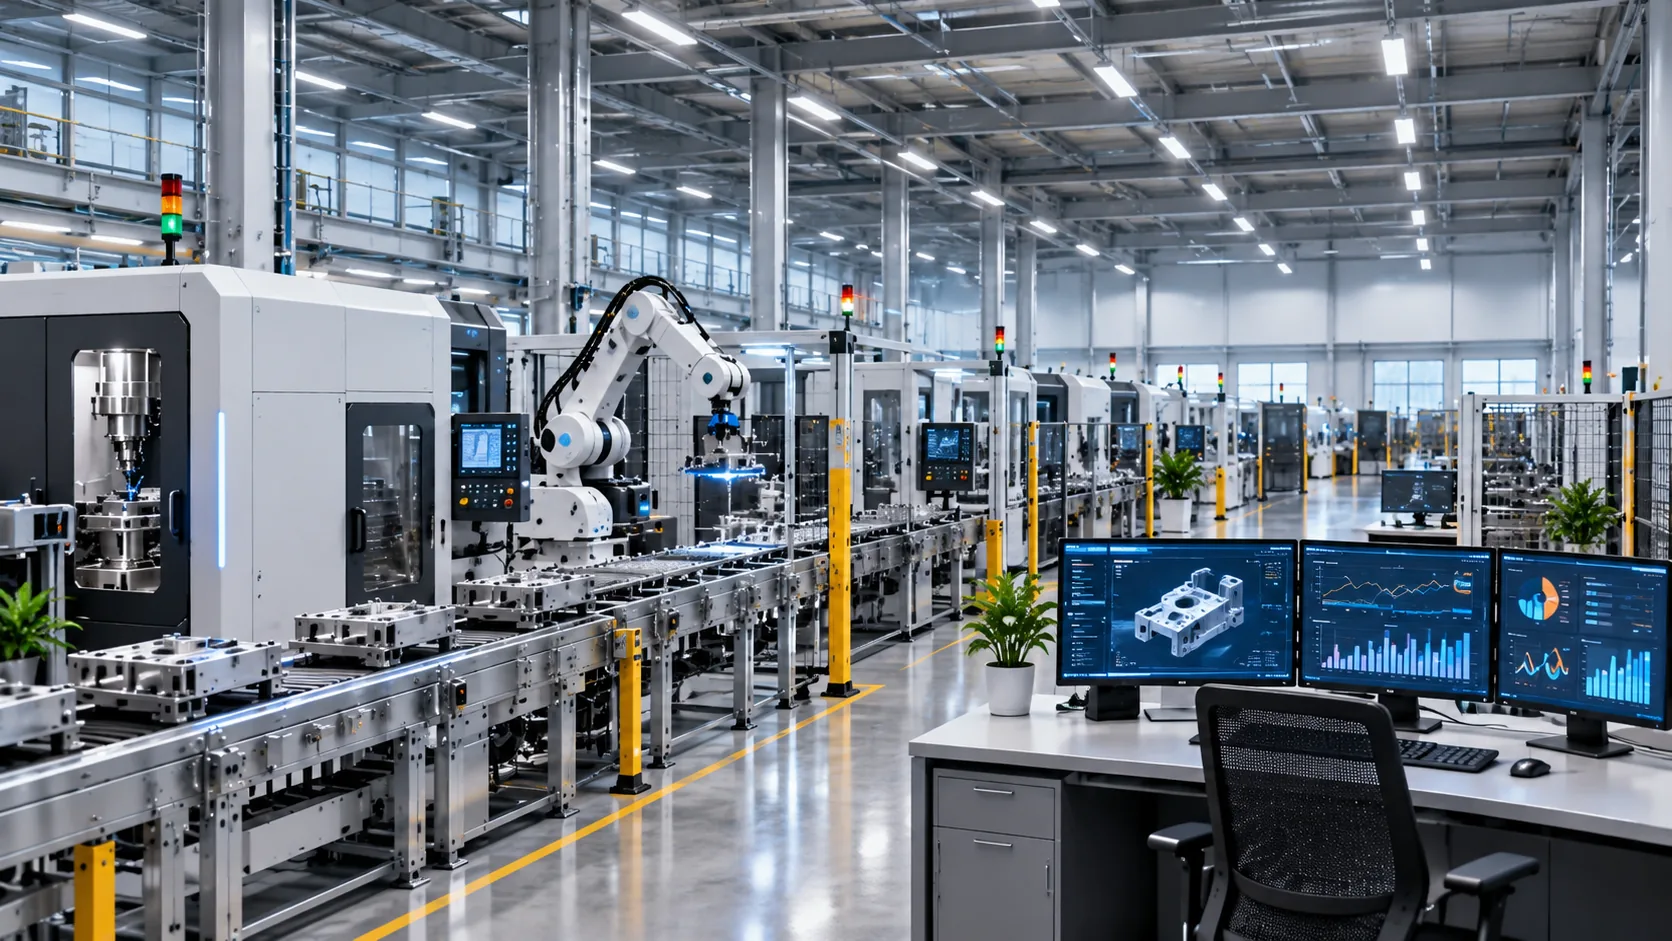
Production Monitoring
MICROCIL's Industrial IoT monitoring approach connects machines, sensors and industrial data sources to a centralized monitoring platform. It transforms available equipment signals into useful information for production teams, maintenance engineers and factory management.
From individual machines to multiple production lines, the solution can be configured around your equipment, data availability and operational priorities.
Tailored solutions for your machines and operations
Connect Existing Machines to an Industrial IoT Platform
Industry 4.0 starts with collecting useful data from equipment and making it available to the people who need it. The architecture depends on the machine interfaces, signals and deployment requirements.
Potential integrations include digital and analog signals, selected sensor interfaces, Modbus RTU over RS485, Modbus TCP and supported PLC/controller data acquisition. Actual compatibility is confirmed during technical assessment.
01. Machines & Shop-Floor Equipment
Existing controllers, PLCs, available signals and selected sensors.
02. Machine Data Acquisition & Edge Connectivity
Signal interfaces, sensors and industrial gateways selected for the application.
03. Industrial Connectivity & Data Communication
Supported wired or wireless connectivity and data transfer.
04. Monitoring Platform & Operational Analytics
Dashboards, alerts, historical data, reporting and operational insights.
Make Production Decisions with Better Operational Visibility
Connected machine monitoring gives production and maintenance teams a more consistent view of equipment activity. Use that information to focus investigations, prioritize attention and make informed operational decisions.
Identify Recurring Downtime
Review stop events and operating history to help investigate repeated interruptions.
Understand Machine Utilization
Track running, idle, and stopped time to see how effectively each machine is being used.
Support Maintenance Planning
Use operating hours and condition trends to plan maintenance before issues lead to breakdowns.
Configure monitoring around the production process, available machine data and the outcomes your team wants to improve.
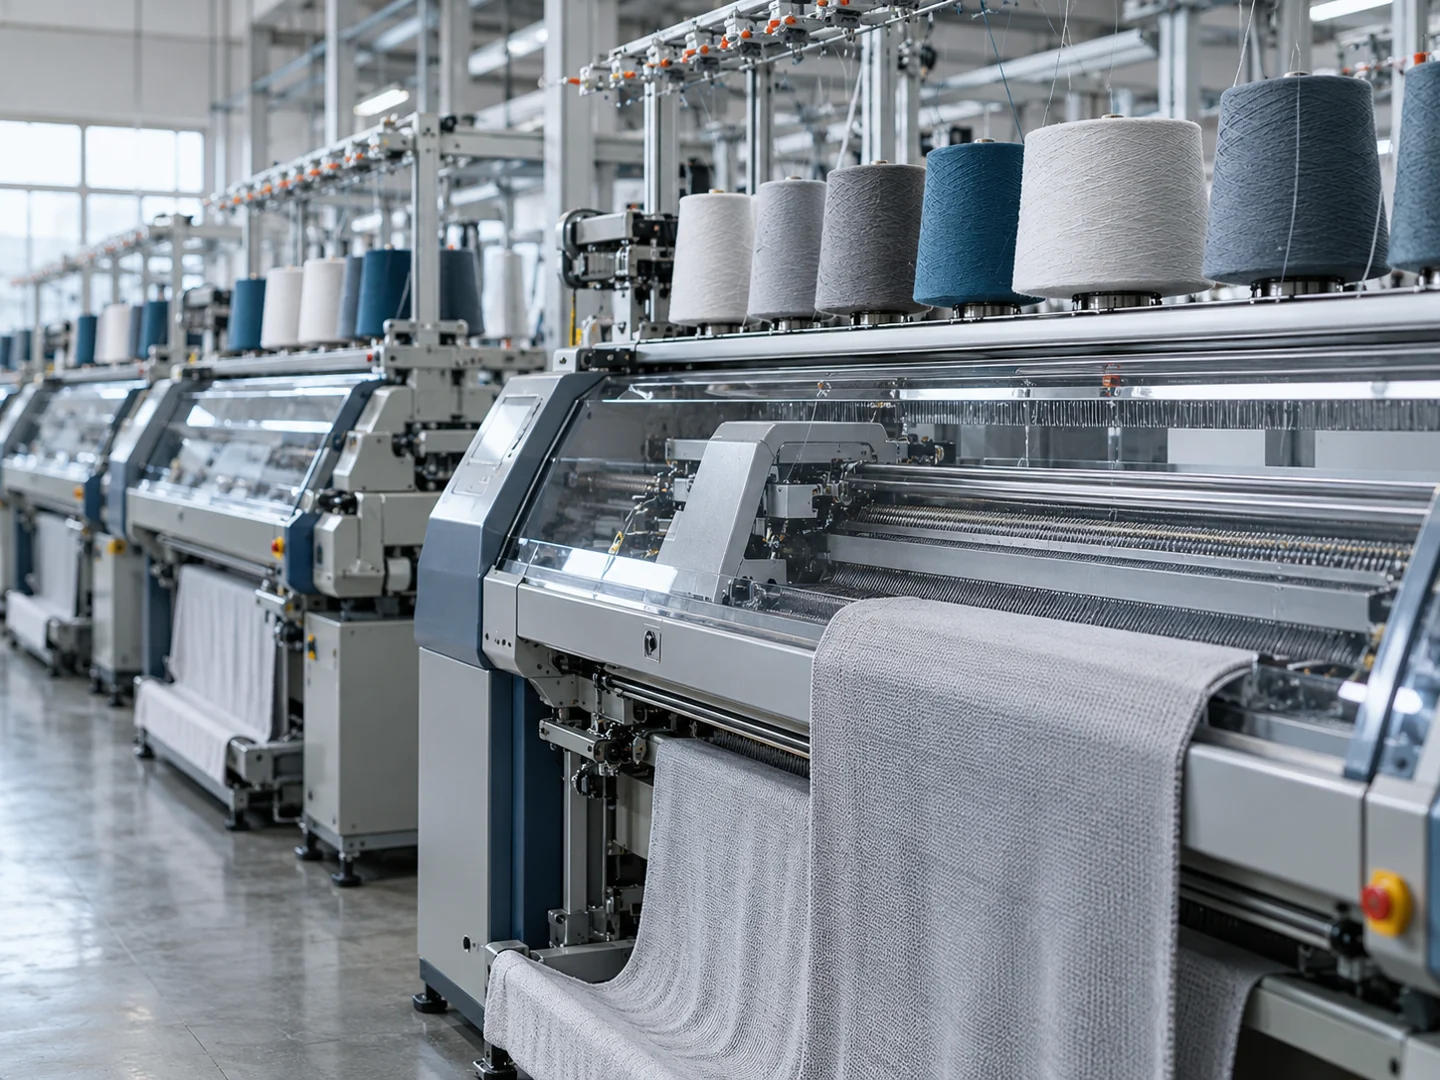
Textile & Knitting Industries
Monitor machine status, running hours, available production counts and downtime events to improve production visibility.
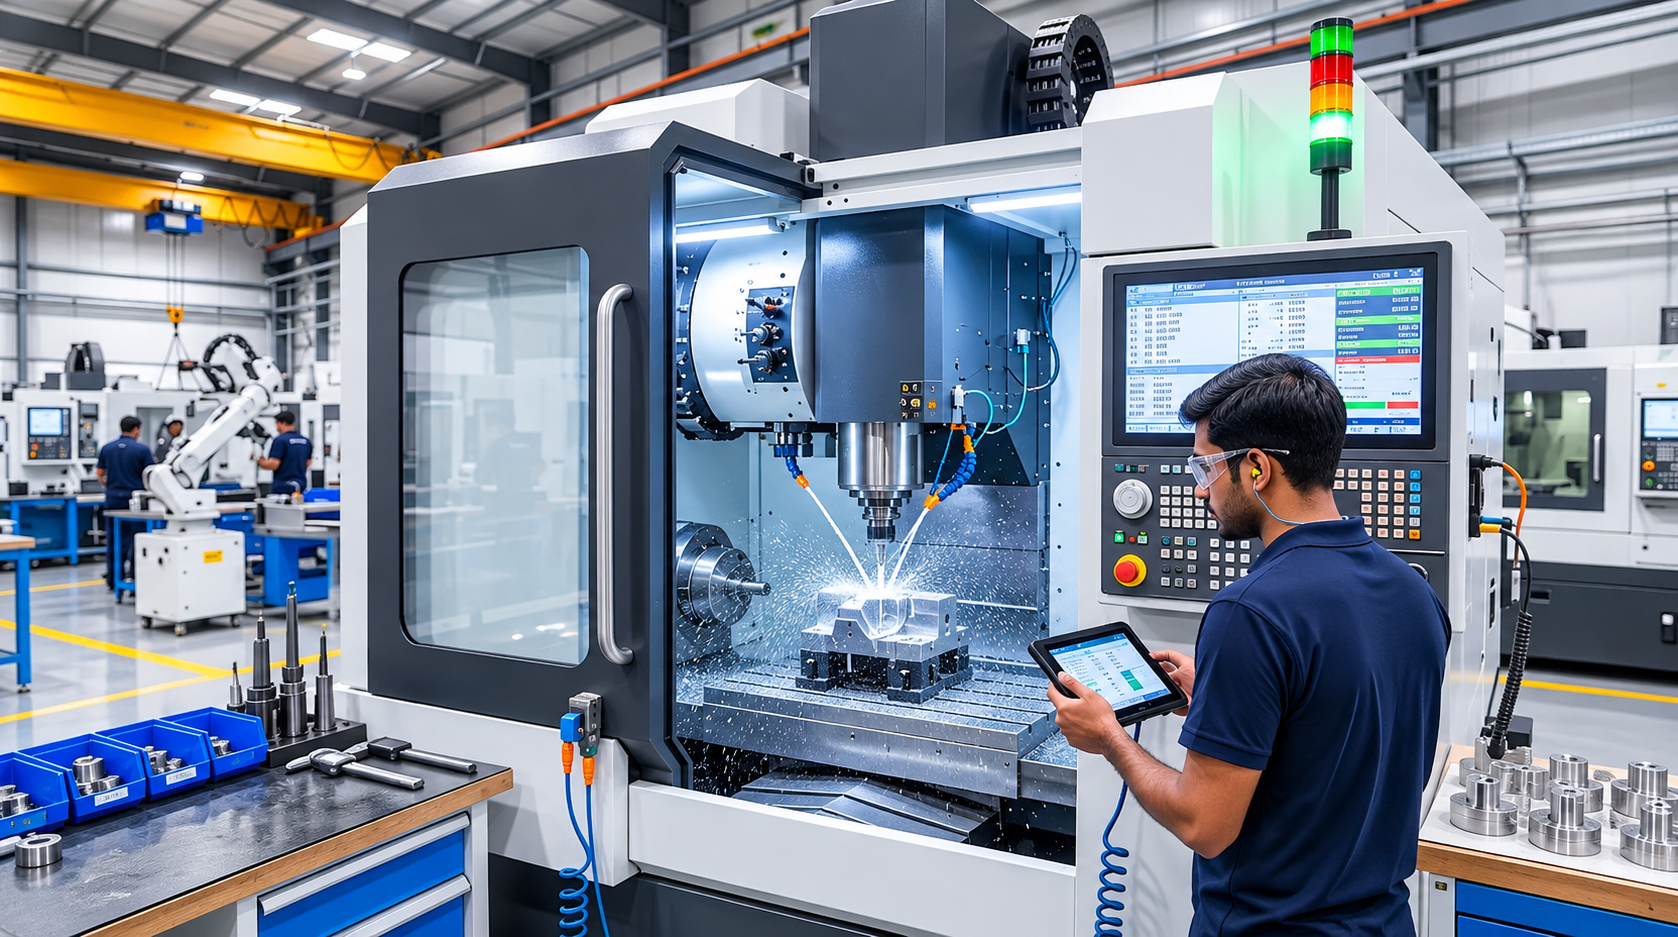
CNC & Precision Manufacturing
Monitor machine activity, cycle-related signals, selected operating parameters and equipment status.
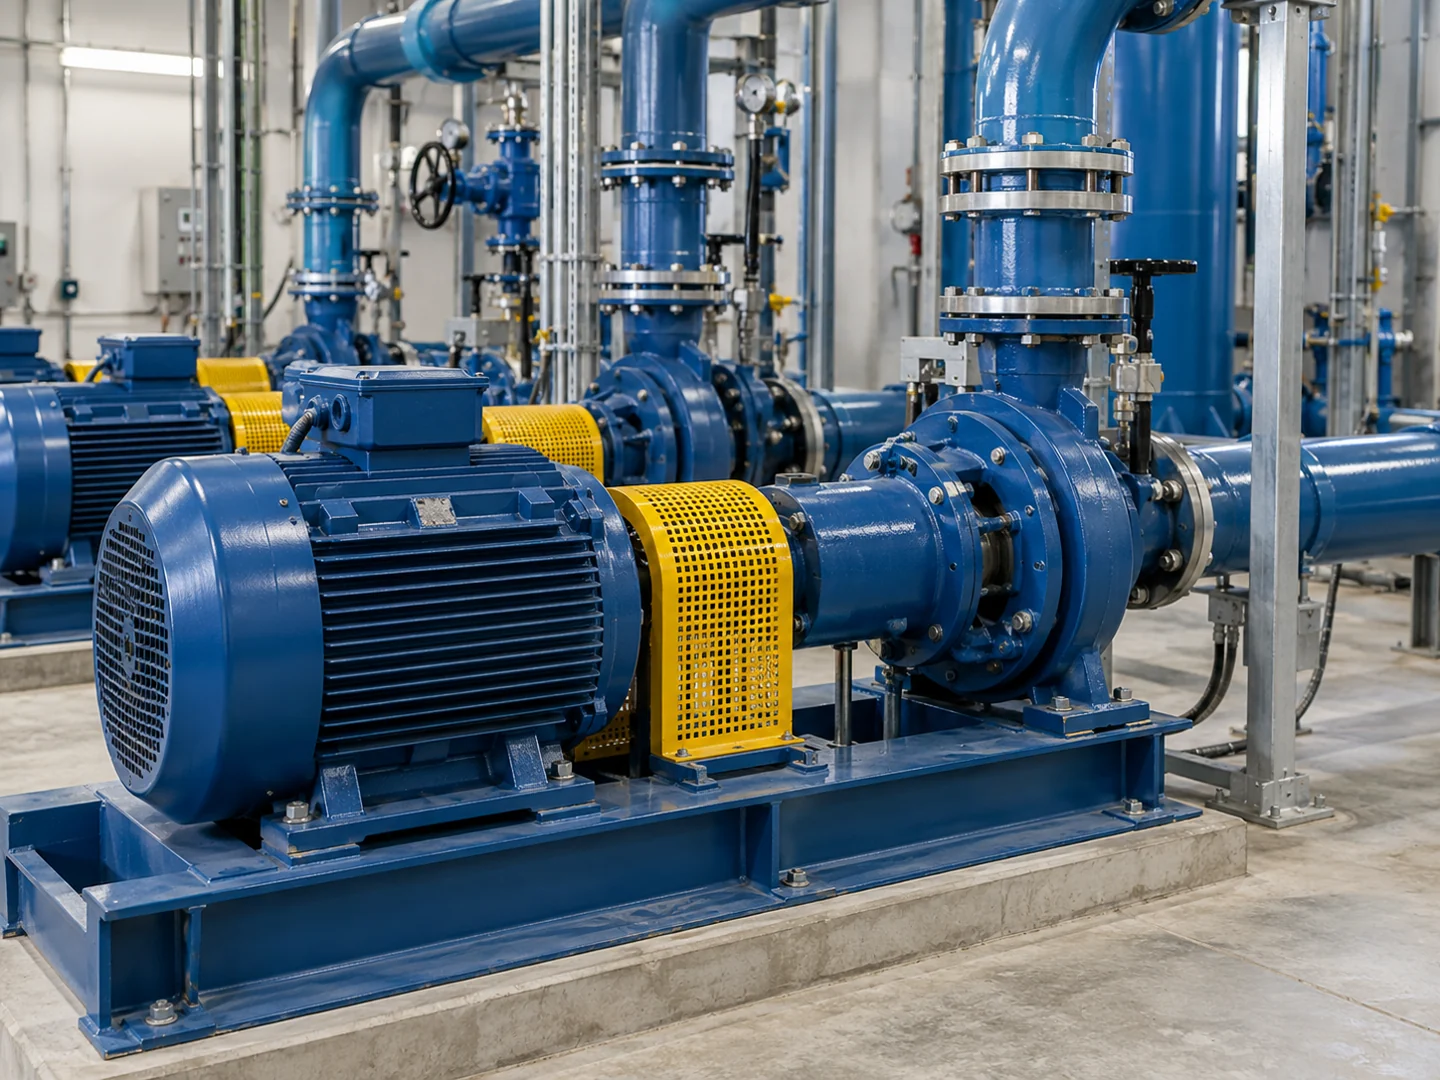
Motors, Pumps & Industrial Equipment
Track operating states and selected condition parameters to support maintenance planning and abnormal-condition alerts.
Manufacturing
Consolidate available machine activity and production signals for a more complete view of connected equipment.
Your Questions, Answered
Quick answers about our Industrial IoT platform, deployment, and results.
What is an industrial machine monitoring system?
An industrial machine monitoring system collects available machine signals and sensor data to provide visibility into operating status, utilization, production activity and selected equipment parameters. It helps production and maintenance teams make decisions using recorded operational information.
What is the difference between machine monitoring and production monitoring?
Machine monitoring focuses on equipment status, operating conditions and utilization. Production monitoring focuses on output, cycle-related information, shift performance and production targets. A connected solution can combine both when the necessary data is available.
Can existing machines be connected to an Industry 4.0 platform?
Often, yes. Depending on the equipment, monitoring may use existing PLC or controller interfaces, digital and analog signals, supported industrial protocols or additional sensors. Each machine should be assessed for compatibility and safe installation.
Can the system monitor machine downtime?
Yes, when appropriate machine-state signals or equivalent data are available. The system can record operating-state transitions and downtime events. Identifying the reason for a stop may require additional signals, operator input or integration with other systems.
Can multiple machines be monitored from one dashboard?
The solution can be designed to consolidate data from multiple connected machines, subject to the deployment scope, supported interfaces and platform configuration.
Does machine monitoring require an internet connection?
Not every monitoring function necessarily requires continuous internet access. The architecture can be designed around local data acquisition and supported connectivity options. Cloud access, remote alerts and centralized reporting depend on the chosen implementation.
Can machine monitoring support predictive maintenance?
Machine monitoring can provide operating histories and condition data that support maintenance analysis. Predictive maintenance requires suitable data, validated methods and, where appropriate, analytical models; it is not automatically guaranteed by basic monitoring alone.
How much does an industrial machine monitoring system cost?
Cost depends on the number and type of machines, required sensors, connectivity, integration effort, dashboard features, data retention and deployment model. MICROCIL can assess the application and prepare a proposal based on the defined scope.
Your machines are already generating data. Let’s turn it into intelligence.
From real-time machine monitoring and production tracking to downtime analysis and equipment health, MICROCIL transforms industrial data into actionable insights for smarter manufacturing operations.
Talk to MICROCIL